Heat Pipe Multi-station Dry-out Tester: Process Guide
1. What Is a Heat Pipe Multi-station Dry-out Tester?
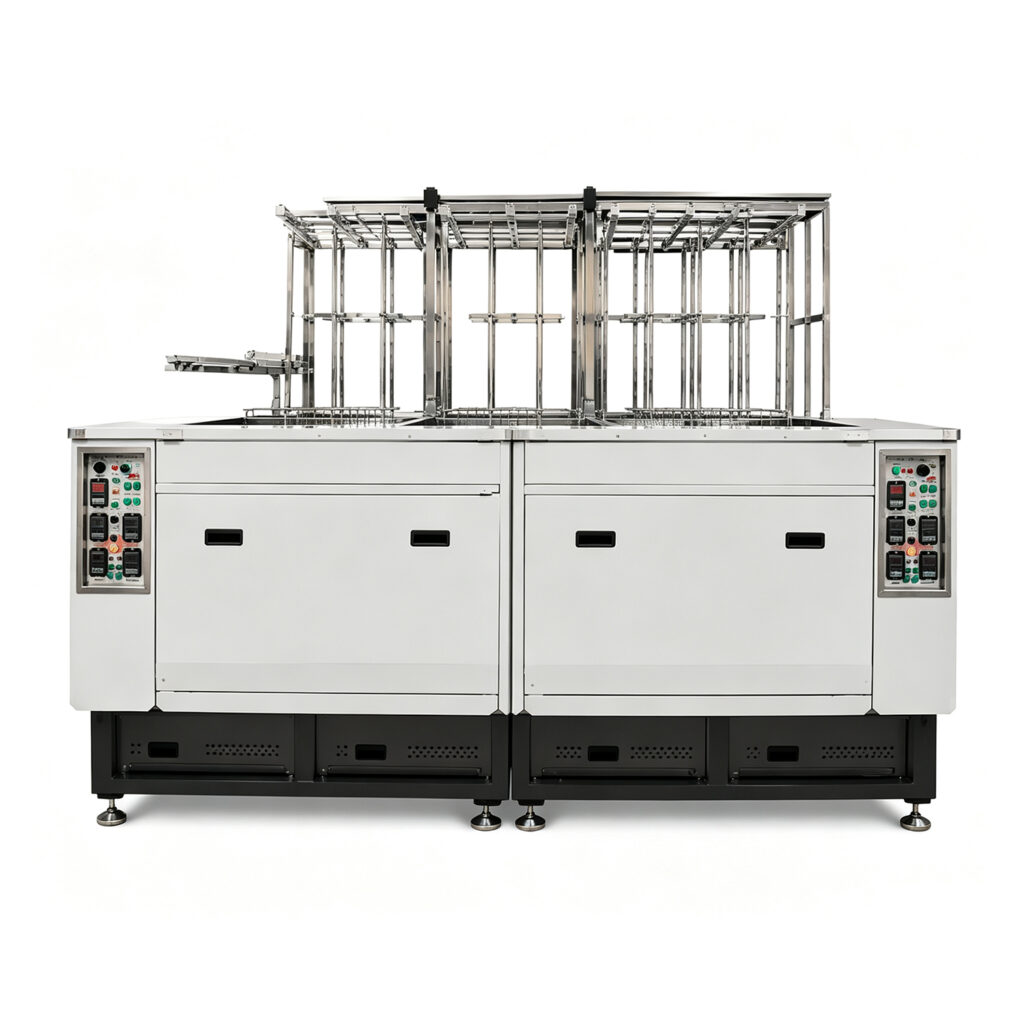
A Heat Pipe Multi-station Dry-out Tester is specialized equipment designed to support controlled drying and process conditioning during heat pipe manufacturing. Depending on its configuration, it may use controlled heating, vacuum assistance, or a combination of process controls to prepare workpieces for subsequent manufacturing stages.
Heat pipes transfer heat through evaporation and condensation inside a sealed enclosure. They commonly contain a metal tube, a working fluid, and an internal wick structure or another liquid-return mechanism.
During operation, the working fluid absorbs heat and evaporates. The vapor travels toward a cooler area and condenses, releasing heat. The liquid then returns toward the heated area, allowing the cycle to continue.
Manufacturing quality directly affects this process. Residual moisture, unwanted contamination, unsuitable fluid charging, or poor sealing can compromise product performance.
A dry-out tester helps manufacturers control a specific part of the production process. Depending on the intended application, it may dry components after cleaning or prepare assembled heat pipes before vacuum processing.
The term “tester” can describe different equipment configurations. Therefore, buyers should confirm whether a particular model performs drying, vacuum-assisted drying, thermal conditioning, or a defined testing operation.
For manufacturers planning a heat pipe production line, the key objective is to establish repeatable processing conditions that match the product design.
2. Why Dry-out Processing Matters in Heat Pipe Manufacturing
Dry-out processing can help prepare heat pipe components for later manufacturing operations. Its exact purpose depends on the materials, assembly condition, and production sequence.
2.1 Removing Residual Moisture
Cleaning processes can leave moisture on workpiece surfaces or inside accessible spaces. If manufacturers do not remove it adequately, moisture may affect subsequent evacuation and charging operations.
Controlled heating can help evaporate residual moisture. However, the appropriate temperature and duration depend on the materials and component design.
A drying cycle must also provide a suitable path for released moisture to escape. Heating alone does not guarantee effective drying in every configuration.
2.2 Supporting Internal Cleanliness
Heat pipes may contain copper tubes, wick structures, and joining materials. Cutting, forming, and assembly can introduce oils, particles, and other residues.
Cleaning should remove the contaminants that the selected process can address. Dry-out processing then helps remove residual moisture or certain volatile substances.
These operations serve different purposes. A dry-out tester cannot replace a validated cleaning procedure or remove every type of contamination.
2.3 Preparing Components for Vacuum Processing
Many heat pipe manufacturing processes require evacuation before working-fluid charging and final sealing.
Residual moisture and material outgassing can influence pressure behavior during evacuation. Properly prepared workpieces may therefore support more consistent downstream processing.
Nevertheless, drying does not replace vacuum evacuation. Manufacturers must verify that the subsequent process meets its required pressure and cleanliness criteria.
2.4 Improving Process Repeatability
Manual drying can introduce variations in temperature, holding time, loading density, and workpiece positioning.
A multi-station dry-out tester can standardize these parameters when it includes suitable controls and validated recipes.
Repeatable settings help manufacturers compare production batches and investigate deviations. Actual performance still depends on equipment condition, loading arrangements, and process validation.
2.5 Protecting Downstream Product Quality
Dry-out processing contributes to manufacturing preparation, but it cannot guarantee finished heat pipe performance by itself.
Working-fluid charging, sealing integrity, internal structure, and thermal design also affect product quality. Manufacturers should establish acceptance criteria for each critical stage.
3. How a Heat Pipe Multi-station Dry-out Tester Works
A typical Heat Pipe Multi-station Dry-out Tester uses controlled processing conditions to remove moisture or prepare workpieces for the next manufacturing operation.
The exact operating principle varies by machine. Some systems use heated stations, while others include vacuum functions or additional monitoring capabilities.
3.1 Workpiece Loading
Operators place the heat pipes or components into designated fixtures.
The fixtures should hold each workpiece securely and provide suitable spacing for consistent processing. Poor loading arrangements may affect heating uniformity or prevent moisture from escaping efficiently.
Manufacturers should define a standard loading pattern for each product family.
3.2 Recipe Selection
The operator selects the approved process recipe through the control interface, if available.
Depending on the equipment, the recipe may include temperature settings, heating time, holding time, and vacuum parameters.
Different materials and heat pipe designs may require different recipes. Manufacturers should validate each recipe before using it for production.
3.3 Controlled Heating
The heating system raises the workpieces or processing chamber to the specified temperature.
Heating can accelerate moisture evaporation and may help release certain volatile substances. The result depends on the temperature, exposure time, material properties, and process environment.
The process must avoid excessive thermal exposure. Sensitive wick materials, coatings, and joining areas may require specific temperature limits.
3.4 Dry-out Holding Period
The machine maintains the specified conditions for a defined period.
Temperature sensors and control logic can help maintain the process recipe. In a multi-station system, the equipment should provide suitable consistency across the occupied stations.
If the machine includes vacuum monitoring, pressure trends may provide additional process information. However, pressure readings alone cannot confirm that every workpiece has reached the required dryness.
3.5 Cycle Completion and Unloading
After the cycle reaches its programmed endpoint, the machine follows its shutdown or cooling sequence.
Operators then transfer the workpieces to the next operation. This may include assembly, vacuum evacuation, fluid charging, or another specified preparation step.
Proper handling and storage help prevent recontamination after drying.
4. Main Components and Technical Features
The configuration depends on the machine’s intended function and production requirements.
Component | Function |
Processing chamber or station assembly | Holds workpieces during processing |
Heating system | Supplies controlled thermal energy |
Temperature sensors | Measures temperature at selected locations |
Workpiece fixtures | Positions products consistently |
Industrial controller | Manages the programmed cycle |
HMI interface | Allows operators to select recipes and monitor status |
Timing controls | Regulates cycle duration |
Safety interlocks | Helps prevent unsafe operation |
Vacuum system, if equipped | Supports reduced-pressure processing |
Pressure sensors, if equipped | Monitors vacuum conditions |
Data logging, if equipped | Records process values and cycle results |
Not every machine includes all these components. Buyers should confirm the actual equipment configuration before comparing suppliers.
4.1 Multi-station Processing Design
Multiple stations allow the machine to accommodate several workpieces or batches within a coordinated process.
The number of stations affects loading capacity and potential throughput. However, a higher station count does not automatically produce higher output.
Heating uniformity, loading time, cycle duration, and downstream capacity also influence production efficiency.
4.2 Temperature Control and Uniformity
Temperature control helps maintain the required drying conditions.
Important specifications include the available temperature range, control accuracy, heating rate, and temperature uniformity under representative loading conditions.
A controller’s setpoint does not necessarily represent the temperature of every workpiece. Manufacturers should request suitable temperature-distribution validation data.
4.3 Programmable Recipes
Recipe management can standardize settings for different product models.
Where supported, the controller may store temperature profiles, cycle durations, and other parameters. Access controls can help prevent unauthorized changes.
A documented recipe system also supports consistent operation across shifts.
4.4 Process Monitoring and Data Recording
Some machines record cycle status, temperature values, alarms, and other process information.
These records can help engineers investigate deviations and compare batches. For effective traceability, manufacturers should link the records to workpiece or batch identifiers.
5. Benefits of Multi-station Dry-out Equipment
5.1 Increased Processing Capacity
Multiple stations can accommodate more workpieces within a coordinated cycle.
This arrangement may reduce the number of separate processing cycles required for a given production volume. Actual capacity depends on the cycle time, loading method, and station layout.
5.2 More Consistent Processing
Automated control can standardize temperature settings and holding times.
This reduces dependence on manual timing and helps operators follow approved procedures. Manufacturers should still verify temperature uniformity and repeatability.
5.3 Reduced Manual Intervention
A programmed cycle can reduce the need for continuous operator supervision.
This may improve workflow efficiency and allow operators to handle other tasks. Actual labor savings depend on loading, unloading, and integration requirements.
5.4 Better Production Traceability
Where data logging is available, manufacturers can review process records and identify recurring deviations.
These records support troubleshooting and continuous improvement. They also help quality teams compare batches when production problems occur.
5.5 Improved Production Coordination
A multi-station tester can support coordinated material flow between cleaning, drying, evacuation, filling, and sealing operations.
This can reduce unnecessary handling and waiting. However, drying capacity must match downstream equipment to avoid creating a new bottleneck.
5.6 Potential Reduction in Process Variation
Standardized recipes and fixtures can help reduce differences between workpieces.
However, variation can also originate from inconsistent cleaning, material conditions, loading patterns, and storage practices. Equipment automation should work alongside effective process controls.
6. Applications in Heat Pipe Manufacturing
A Heat Pipe Multi-station Dry-out Tester may support different manufacturing stages, depending on the machine’s verified capabilities.
6.1 Copper Heat Pipe Preparation
Copper heat pipes are widely used in electronics cooling and thermal management systems.
After cutting, forming, or cleaning, selected components may require drying before assembly or vacuum processing.
The drying procedure should suit the copper tube, wick structure, and other materials involved.
6.2 Wick Structure Preparation
Some wick manufacturing processes include cleaning or moisture-sensitive preparation steps.
A suitable drying system may support these stages before assembly or further processing. The required conditions depend on the wick material and manufacturing method.
6.3 Heat Pipe Assembly Preparation
Assembled heat pipes may require controlled drying or conditioning before evacuation and working-fluid charging.
The machine must accommodate the assembly’s dimensions and material limits. Manufacturers should validate the process using representative workpieces.
6.4 High-volume Production
Multi-station processing may suit factories producing repeated batches of similar heat pipes.
Standardized fixtures and recipes can help maintain consistency. For high-mix production, manufacturers should also evaluate changeover time and recipe management.
6.5 Thermal Management Components
Heat pipes serve applications in laptops, telecommunications equipment, power electronics, and other thermal management systems.
A dry-out tester supports manufacturing preparation rather than directly confirming final thermal performance. Finished products still require appropriate quality checks.
7. How to Choose the Right Dry-out Tester
Equipment selection should begin with the product requirements and intended process function.
7.1 Confirm the Machine’s Purpose
Determine whether the equipment performs component drying, assembled heat pipe drying, vacuum-assisted drying, or another process operation.
Suppliers may use the term “dry-out tester” differently. Ask for a process description and confirm the actual functions included.
7.2 Define Workpiece Dimensions
Prepare drawings showing the heat pipe dimensions, materials, shapes, and loading requirements.
Consider the tube length, diameter, wall thickness, and fixture arrangement. The equipment must accommodate the intended product range without compromising processing consistency.
7.3 Evaluate Temperature Performance
Confirm the temperature range, control accuracy, heating rate, and uniformity.
Ask how the supplier verifies temperatures under representative production loads. Also confirm whether the process can protect sensitive materials from excessive thermal exposure.
7.4 Determine the Required Station Count
Choose the number of stations based on target output and cycle time.
Consider loading, heating, holding, cooling, unloading, and changeover time. Request a throughput estimate that reflects the actual production workflow.
7.5 Verify Vacuum Functions
If vacuum assistance is required, confirm the pressure range, pump configuration, pressure measurement capability, and operating sequence.
Do not assume every multi-station dry-out tester includes a vacuum system.
7.6 Review Controls and Data Features
Determine whether the machine supports programmable recipes, alarms, data recording, and production reporting.
For traceable manufacturing, confirm how cycle records can be linked to specific batches or workpieces.
7.7 Consider Maintenance and Safety
Review sensor calibration, heating-element maintenance, fixture wear, electrical safety, and operator access.
Ask the supplier for maintenance schedules, spare-parts information, operating instructions, and training requirements.
7.8 Compare Total Operating Costs
The initial purchase price is only one factor.
Evaluate energy use, maintenance, consumables, labor, floor space, and potential downtime. The best choice should meet the process requirements while supporting sustainable operating costs.
8. Quality Control and Process Optimization
A reliable dry-out process requires defined parameters and measurable acceptance criteria.
8.1 Establish Temperature and Time Limits
Set the approved temperature profile and holding time for each product family.
These values should come from process development and validation. Avoid applying one universal recipe to different heat pipe designs.
8.2 Verify Temperature Uniformity
The controller’s sensor may not reflect the temperature at every station.
Manufacturers should evaluate representative loading patterns and confirm temperature distribution using suitable measurement methods.
This helps identify cold spots and uneven heating.
8.3 Standardize Loading
Workpiece spacing and fixture position can affect heating and moisture removal.
Use a documented loading pattern for each product family. If the batch quantity or fixture arrangement changes, assess whether the process needs revalidation.
8.4 Prevent Recontamination
After drying, workpieces can collect contaminants or absorb moisture during handling and storage.
Use suitable transfer procedures and storage conditions to maintain the required state before downstream processing.
8.5 Maintain Equipment Calibration
Temperature sensors, pressure sensors where fitted, and control systems should be checked according to a documented maintenance plan.
Calibration records support process consistency and help identify measurement errors.
8.6 Verify Downstream Quality
A completed dry-out cycle does not guarantee finished heat pipe performance.
Manufacturers should verify vacuum evacuation, working-fluid charging, sealing, leak integrity, and thermal performance according to the product specification.
9. Common Problems and Solutions
Problem | Possible cause | Recommended action |
Inconsistent drying results | Uneven heating or different initial moisture levels | Verify loading, temperature distribution, and upstream cleaning |
Excessive cycle time | Unsuitable recipe or insufficient heating capacity | Review cycle data and validate the process under realistic loads |
Different results between stations | Uneven heating or sensor placement | Measure representative workpiece temperatures and inspect fixtures |
Workpiece discoloration | Excessive temperature or surface contamination | Review the temperature profile and material preparation |
Results vary between batches | Inconsistent cleaning, storage, or recipe selection | Standardize handling and verify approved recipes |
Moisture returns after drying | Recontamination or unsuitable storage | Review cooling, transfer, and storage procedures |
Frequent machine alarms | Sensor faults or operation outside approved limits | Review alarm records and follow the maintenance procedure |
These symptoms can have several causes. Engineers should investigate the process systematically before changing operating parameters.
10. Integration Into a Heat Pipe Production Line
A Heat Pipe Multi-station Dry-out Tester may form part of a broader heat pipe manufacturing workflow.
A typical process may include:
- Tube cutting and material preparation.
- Forming and wick structure preparation.
- Cleaning and rinsing.
- Drying or dry-out processing.
- Assembly and joining.
- Vacuum evacuation.
- Working-fluid charging.
- Final sealing.
- Leak testing.
- Thermal performance testing.
The actual sequence depends on the heat pipe design and the stage at which drying is required.
10.1 Integration With Cleaning Equipment
Cleaning removes contaminants, while drying helps remove residual moisture.
These processes should be designed together. A dry-out tester cannot reliably compensate for inadequate cleaning.
Suggested internal link: Heat Pipe Equipment Production Line.
10.2 Integration With Vacuum Filling Equipment
Drying may prepare workpieces for vacuum evacuation and working-fluid charging.
The production workflow should minimize exposure to moisture and contamination between operations.
Suggested internal link: Heat Pipe Filling & Welding Machine.
10.3 Integration With Thermal Testing Equipment
After filling and sealing, finished heat pipes may require leak testing and thermal performance evaluation.
These tests measure different aspects of product quality. Dry-out processing cannot replace finished-product verification.
Suggested internal link: Heat Pipe Thermal Performance Tester.
10.4 Production Data Integration
If the machine supports data recording, dry-out results can be linked to downstream process records.
This helps manufacturers trace quality issues and compare batches. Effective implementation requires reliable product identification and consistent record management.
11. Frequently Asked Questions
11.1 What is a Heat Pipe Multi-station Dry-out Tester?
It is equipment designed to support controlled drying, heating, or process conditioning across multiple workstations during heat pipe manufacturing. Its exact functions depend on the machine configuration.
11.2 Why is dry-out processing important?
Dry-out processing can help reduce residual moisture and certain volatile contaminants before subsequent manufacturing steps. It supports preparation but does not replace cleaning, vacuum evacuation, filling, or sealing.
11.3 Does every dry-out tester include a vacuum system?
No. Some machines use controlled heating without vacuum assistance. Others combine heating with vacuum processing. Buyers should confirm the available functions and technical specifications.
11.4 How many stations should a manufacturer choose?
The required station count depends on production volume, cycle time, workpiece dimensions, and loading method. Compare actual throughput rather than selecting the highest station count automatically.
11.5 What temperature should be used?
There is no universal temperature for all heat pipes. The appropriate profile depends on the materials, wick structure, assembly condition, and process objective.
11.6 Can a dry-out tester improve heat pipe thermal performance?
It can support manufacturing quality by helping control moisture and preparation conditions. Finished thermal performance also depends on the wick structure, working-fluid charge, internal cleanliness, sealing integrity, and product design.
11.7 What is the difference between dry-out testing and thermal performance testing?
Dry-out processing prepares workpieces under controlled conditions. Thermal performance testing evaluates heat transfer under defined test conditions.
11.8 What information should buyers provide for a quotation?
Provide workpiece dimensions, materials, loading quantity, process purpose, required temperature range, target cycle time, vacuum requirements if applicable, and automation preferences.
11.9 Can the machine handle different heat pipe sizes?
It may, provided the fixtures, processing chamber, heating system, and control recipes support the required range. Confirm changeover procedures and validation requirements with the supplier.
11.10 How should the equipment be maintained?
Maintenance may include checking heating elements, temperature sensors, fixtures, electrical connections, safety interlocks, and vacuum components where fitted. Follow the manufacturer’s maintenance schedule and record the checks.
12. Conclusion
A Heat Pipe Multi-station Dry-out Tester can support controlled drying and process preparation in heat pipe manufacturing. Multiple stations may help manufacturers process workpieces efficiently while maintaining defined operating conditions.
The right equipment depends on the product design, required drying conditions, station capacity, temperature control, and production integration needs. Buyers should confirm the machine’s actual functions and validate the process using representative workpieces.
Dry-out processing remains one stage of the complete manufacturing workflow. Cleaning, vacuum evacuation, working-fluid charging, sealing, leak testing, and thermal performance testing all contribute to finished-product quality.
For manufacturers upgrading their heat pipe production capacity, cncoolingthermal can be referenced as the brand associated with the website’s thermal manufacturing equipment offerings. Confirm the available machine specifications, station configurations, and customization options against the actual equipment range.