Product Description
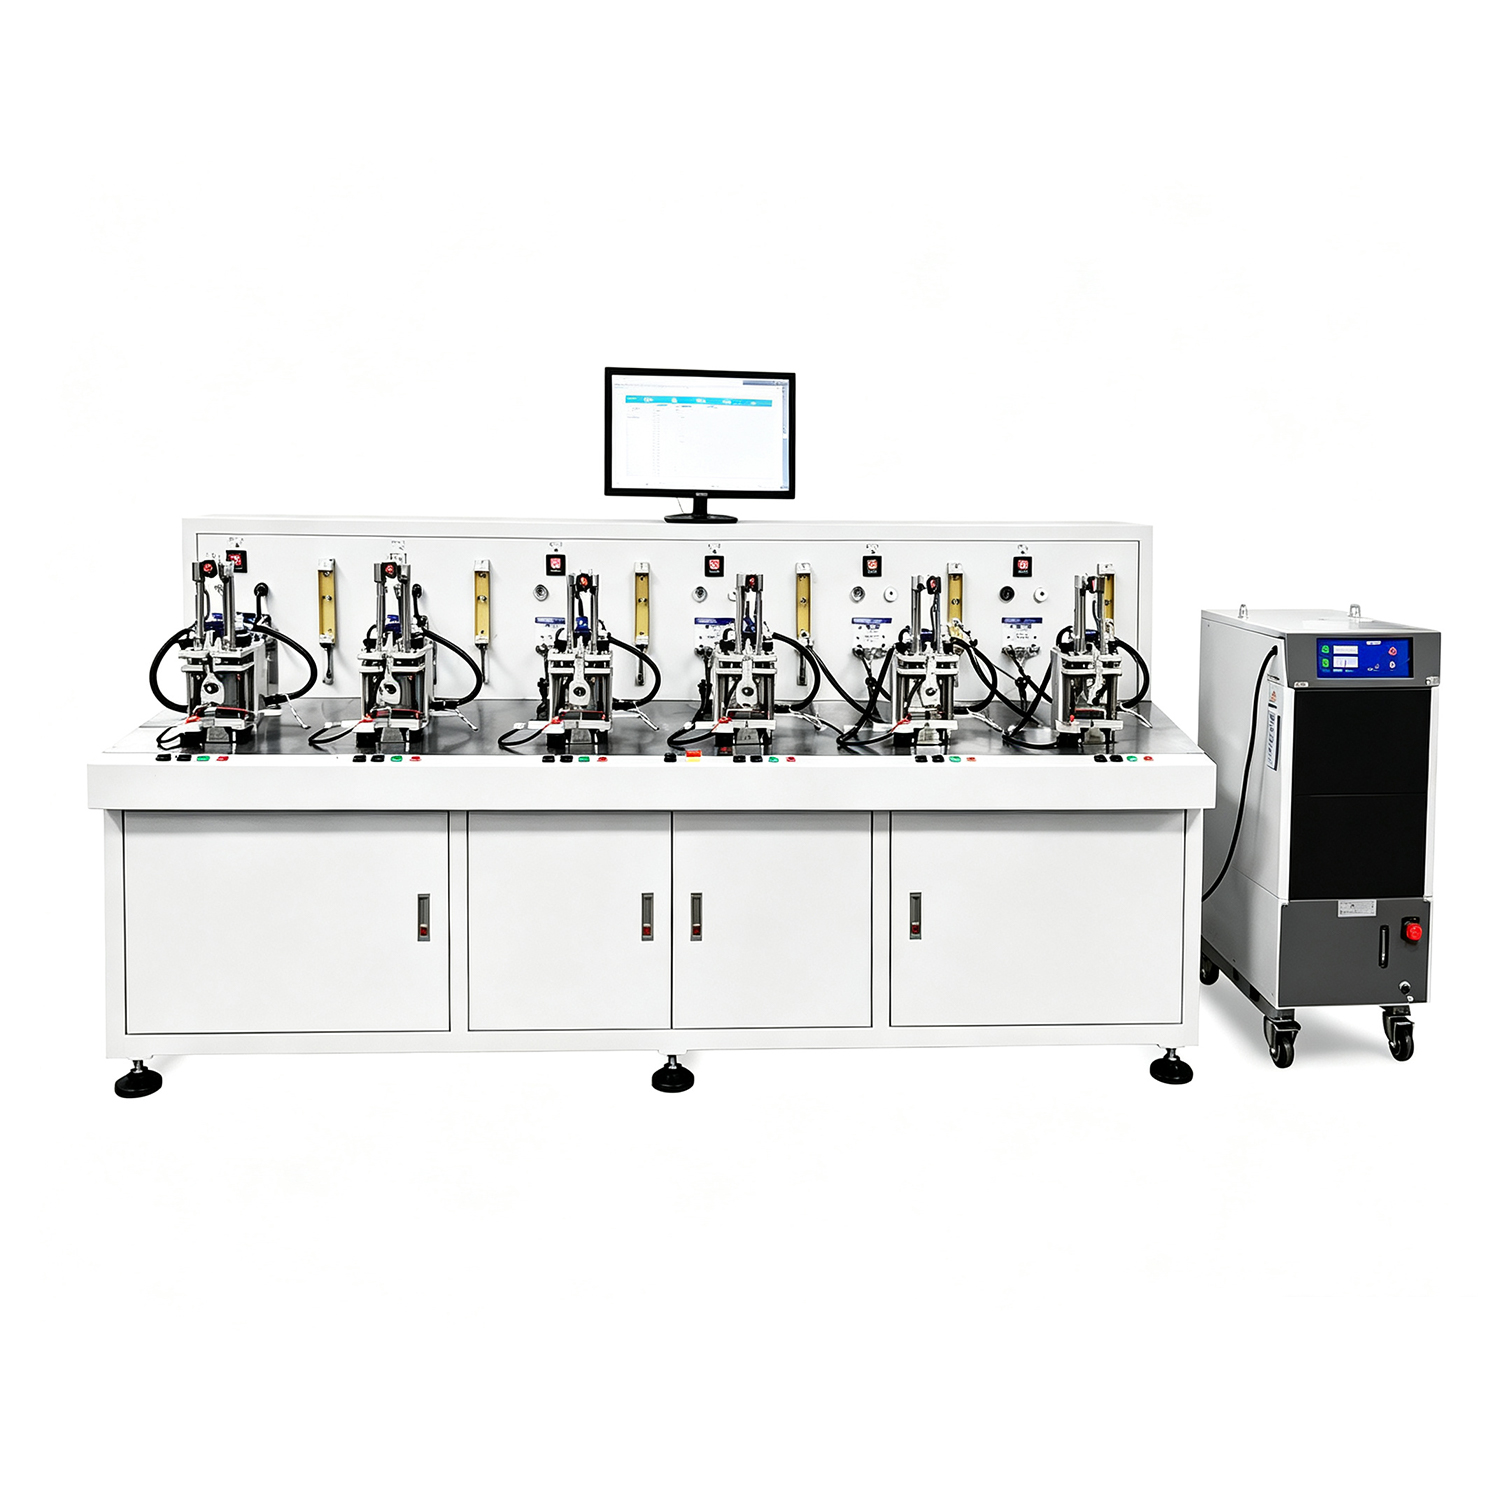
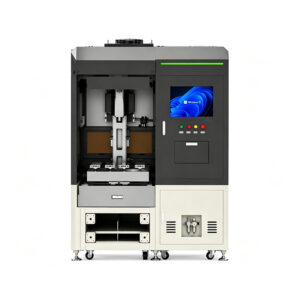
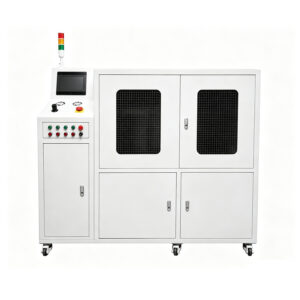
A heat pipe that passes leak testing and passes dimensional inspection is still not a verified heat pipe — it is a sealed copper tube with working fluid inside. The only way to confirm that the sintered wick, working fluid charge, and vacuum level are all correct is to measure the heat pipe’s thermal performance under controlled, repeatable test conditions. Cooling-Thermal’s Automatic Heat Pipe Performance Testing Machine is the Step 11 quality gate of the complete heat pipe production line — the machine that measures Qmax, thermal resistance (R-value), and ΔT of every heat pipe before it leaves the production line, at 250 pieces per hour, across the full range of 2D and 3D heat pipe geometries used in CPU coolers, laptop thermal modules, server cooling assemblies, and AI thermal management systems.
Equipment Specifications
| Specification | Standard Model | Advanced Model |
|---|---|---|
| Workstations | 6 stations | 6 stations |
| Production Capacity | 250 pcs/hr | 240 pcs/hr (≤60s/test) |
| Max Test Power | 90 ± 0.25W | ≤ 200W |
| Heating End Size | 15 × 15 × 30 mm | 15 × 130 × 150 mm |
| Cooling Area | — | 27 × 130 × 150 mm |
| Maximum Test Area | 70 × 170 mm | — |
| Heat Source | Single heat source | Single heat source |
| Temperature Points | 3+1 (hot plate) / 2+1 (heat pipe) | 3 measurement points |
| Test Angles | Horizontal, vertical | Horizontal, vertical |
| Test Pressure | Air pressure adjusted | — |
| Test Shape | 2D stackable | 2D, 3D |
| Cooling System | — | 5L/min, 25–40°C, ±1°C |
| Flowmeter | — | ≤ 250 CC/min (controllable) |
| Software | — | LabView |
| Pipe Diameter | Ø5 – Ø10 mm | Ø5 – Ø10 mm |
| Pipe Length | ≤ 500 mm | ≤ 500 mm |
| Applicable Shapes | 2D, 3D | 2D, 3D |
| Voltage / Power | 220V × 1φ × 8 kW | 220V × 1φ × 8 kW |
| Dimensions | 1,725 × 1,080 × 1,650 mm | 2,000 × 1,200 × 1,600 mm |
| Weight | — | 700 kg |
What the Heat Pipe Performance Testing Machine Measures — Qmax, Thermal Resistance, and ΔT Explained
Qmax — Maximum Heat Transport Capacity
Qmax is the maximum power (in Watts) that a heat pipe can transport from its evaporator section to its condenser section without dry-out — without the sintered wick running out of liquid working fluid at the evaporator due to insufficient capillary pumping force to return condensed fluid from the condenser. In production testing, Qmax is determined by stepwise increasing the heater power at the evaporator end while monitoring the evaporator temperature: Qmax is reached when the evaporator temperature rises sharply (indicating dry-out onset) rather than increasing proportionally with power. The standard model’s 90W test power and the advanced model’s 200W test power define the maximum Qmax that can be characterised — appropriate for the 5–50W Qmax range of standard Ø4–Ø8mm sintered wick heat pipes used in electronics cooling.
Thermal Resistance (R-value)
Thermal resistance R = ΔT / Q — the temperature difference between the evaporator and condenser divided by the heat power applied. R is the single number that quantifies how effectively a heat pipe moves heat: lower R means better thermal performance. In production testing, R is measured at the rated test power (not at Qmax) — the thermal resistance under the normal operating condition the heat pipe will experience in its application. The advanced model’s 3 temperature measurement points (at precisely defined locations on the evaporator, adiabatic, and condenser sections) enable the R calculation with the spatial resolution required for server and AI cooling heat pipe qualification.
ΔT — Temperature Difference
ΔT (delta T) is the temperature difference between the heater block (simulating the CPU or component heat source) and the condenser end (simulating the heat sink or cold plate). In production testing, ΔT is the pass/fail criterion: each heat pipe is tested at the defined test power, and units where ΔT exceeds the specified maximum are rejected. The machine’s automatic OK/NG judgement function applies this criterion at full production speed — 250 pieces per hour — without operator interpretation, eliminating inter-operator variability from the quality gate.
A heat pipe that fails the performance test is a heat pipe that will fail in the customer’s product. Catching it at Step 11 costs one heat pipe. Missing it costs a field return, a warranty claim, and a customer relationship.
Step 11 in the Heat Pipe Production Line — Why Performance Testing Is the Final Quality Gate
| Step | Equipment | What It Verifies |
|---|---|---|
| 1 | Automatic Pipe Cutting Machine | Length ±0.10mm |
| 2 | Pipe Shrinking Machine | End geometry |
| 3 | Copper Powder Filling Machine (4,000 pcs/hr) | Wick powder bed |
| 4 | Vacuum Sintering Furnace (850–1000°C) | Wick bond strength |
| 5 | Degassing & Water Injection Machine | NCG level + fluid charge |
| 6 | Automatic Welder (550 pcs/hr) | Seal integrity |
| 7 | Hot Press Machine (±0.05mm, 15t) | Flatness ±0.05mm |
| 8 | Automatic Bending Machine (99% yield) | Bend geometry |
| 9 | Heat Pipe Straightening Machine (±0.2mm) | Parallelism |
| 10 | Helium Leak Testing Machine (1,000 pcs/hr) | Seal leak rate |
| 11 | Heat Pipe Performance Testing Machine (250 pcs/hr) | Qmax + ΔT + R-value |
Steps 1–10 verify that the heat pipe was built correctly. Step 11 verifies that it works correctly. A heat pipe can pass every dimensional inspection and leak test and still fail performance testing — if the sintered wick has voids from a powder filling problem, if the working fluid charge is outside the ±0.05g tolerance, or if the vacuum level is insufficient due to a borderline degassing result. Performance testing at Step 11 catches these failure modes that earlier steps cannot detect because they require the heat pipe to operate as a two-phase thermal device under controlled heat load conditions.
Applications — Which Heat Pipe Products Require Performance Testing and Which Model to Choose
- CPU cooler heat pipes (Ø6–Ø8mm, 2D flat, 5–35W Qmax): Standard (90W, 250pcs/hr) — ΔT at rated power, Qmax, R-value
- Laptop thermal modules (Ø4–Ø6mm, 3D, ultra-thin): Standard (2D/3D stackable) — ΔT auto-OK/NG, 60s cycle
- High-performance laptop (Ø6mm, multi-bend 3D, 30–50W): Advanced (200W, LabView) — Full R-value curve, Qmax, data log
- Server rack cooling (Ø8–Ø10mm, 3D, 50–150W Qmax): Advanced (200W, cooling water) — R-value at multiple power levels
- AI server / GPU cooling (Ø8–Ø10mm, 80–200W): Advanced (200W, LabView + flowmeter) — Full thermal characterisation, traceability
- EV battery thermal management (Ø6–Ø10mm, custom 3D): Advanced (LabView data export) — R-value certification data
- Mixed production line (multiple OD/geometry): Standard (quick changeover) — Per-product OK/NG limit setting
Why Choose Cooling-Thermal— Specialist Thermal Solution Production Line Knowledge
1. Parameters Set Against Real Heat Pipe Thermal Specifications
General thermal test equipment manufacturers specify their machines against generic test standards.Cooling-Thermal’s performance testing machines are specified against the actual Qmax, R-value, and ΔT specifications of heat pipes produced at Foxconn, Nidec, Furukawa Electric, and Cooler Master — manufacturers whose heat pipe thermal specifications define the industry benchmark. Our test power range (90W standard / 200W advanced), heater dimensions (15×15mm / 15×130mm), and cooling water parameters (25–40°C, ±1°C) are not arbitrary — they are the parameters required to accurately characterise the Qmax and R-value of the specific Ø4–Ø10mm sintered wick heat pipes these manufacturers produce.
2. Complete Line Accountability — We Know What Causes Performance Failures
Cooling-Thermal supplies every machine in the heat pipe production line from Step 1 to Step 11. When a production line’s performance testing station shows elevated rejection rates, our engineers can trace the root cause across every upstream production step — powder filling density variation at Step 3, vacuum level at Step 5, working fluid charge tolerance at Step 5 — because we built and commissioned all of them. This complete-line knowledge is why Cooling-Thermal’s performance testing machines are calibrated with pass/fail limits that correctly reflect the upstream process capability, not generic limits that produce unacceptably high rejection rates on good product.
3. LabView Integration — Production Data That Meets Tier-1 Customer Requirements
Foxconn, Nidec, and Furukawa Electric require full thermal characterisation data — not just a pass/fail result — for heat pipe qualification and ongoing production monitoring. The advanced model’s LabView software generates the complete test dataset: temperature vs time curves, power stability records, R-value trend across production batches, and individual heat pipe test records with batch number and station ID. This traceability data is what Tier-1 electronics manufacturers require for their incoming quality control and thermal design validation processes.
Cooling-Thermal vs Generic Thermal Test Equipment — Why Production-Line Testers Are Different from Lab Instruments
| Cooling-Thermal Performance Tester | Generic Lab Thermal Analyser | Manual Test Fixture | |
|---|---|---|---|
| Throughput | 250 pcs/hr — production line speed | 1–5 pcs/hr — lab measurement speed | 10–30 pcs/hr — operator dependent |
| OK/NG judgement | Automatic, real-time, per-unit | Manual data interpretation | Manual — operator variation |
| Data logging | LabView: full dataset + batch traceability | Lab software, not production format | Paper/spreadsheet — no traceability |
| Heat pipe geometry | 2D + 3D, stackable fixture | Custom jig per product — costly | Custom jig — operator setup |
| Test angles | Horizontal + vertical, auto | Single fixed angle typically | Manual repositioning |
| Cooling water | 5L/min, 25–40°C ±1°C (advanced) | Separate chiller required | No controlled cooling |
| Production integration | Step 11 of Cooling-Thermal 11-step line | Standalone lab instrument | Standalone station |
| Validated by | Foxconn, Nidec, Furukawa, Cooler Master | Research institutions | In-house only |

Heat Pipe Loading and Positioning

Thermal Conditioning

Data Recording and OK/NG Judgement

Reviews
There are no reviews yet.