Product Description
Overview
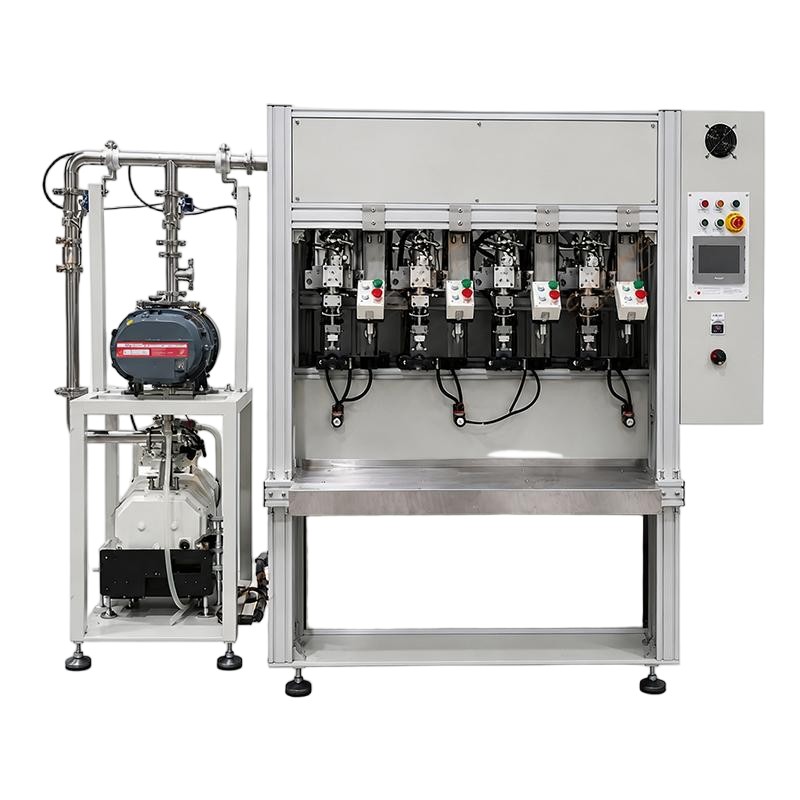
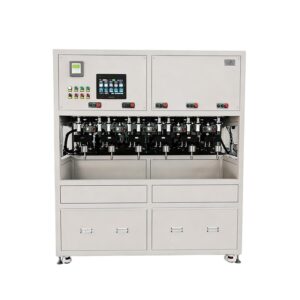
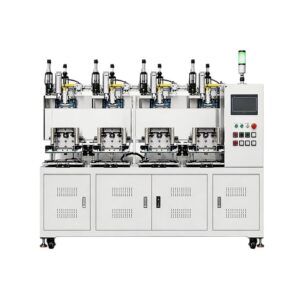
An automatic heat pipe production line takes a copper pipe that already has its wick and working fluid loaded, and carries it through the remaining critical steps — degassing, sealing, and testing — without manual transfer between stations. Each station is synchronized by a shared PLC, so cycle time is set by the slowest station rather than by however fast an operator can carry parts between six separate machines.
| Parameter | Specification |
|---|---|
| Pipe Diameter Range | Ø4–Ø10mm |
| Pipe Length Range | 80–500mm |
| Line Stations | Tail welding, water/fluid filling, primary vacuum degassing, secondary heating degassing, fixed-length cutting, head welding, testing |
| Control System | Central PLC with touchscreen HMI, station-by-station status display |
| Vacuum Level | 10⁻² to 10⁻³ Torr class, station-dependent |
| Sealing Method | TIG / argon arc tail and head welding |
| Testing Included | In-line temperature/thermal performance check per pipe |
| Data Logging | Vacuum level, weld parameters, and test result recorded per pipe |
Key Advantages of an Integrated Production Line
Lower Labor Cost Per Pipe
Running degassing, sealing, and testing as separate standalone machines means an operator at every station and a handling step between each one. On an integrated line those steps run back to back under one control system, and a properly staffed line typically lets a single operator oversee two lines running in parallel rather than one operator per machine.
Fewer Handling-Induced Defects
Every time a thin copper pipe is unclamped and re-fixtured at a new station, there is a chance of a dent, a scratch, or a fixture misalignment that shows up later as a leak or a cosmetic reject. An integrated line clamps the pipe once and carries it through the sequence, cutting the number of handling touches per pipe.
Consistent Vacuum Integrity from Degassing to Sealing
Secondary degassing only does its job if the pipe stays under vacuum through to the weld. Because the line moves the pipe directly from the degassing station to head welding without exposing it to atmosphere in between, it closes the gap that shows up when degassing and welding run as separate, disconnected machines.
Full Batch Traceability
Vacuum level, weld current and duration, and the final test result are logged against every pipe as it moves down the line, which gives your quality team a complete record per batch instead of a spot-checked sample.
How the Line Works
Stage 1: Tail Welding & Water Filling
The pipe, already loaded with wick and powder, is loaded into the fixture. The tail is sealed by TIG welding, then a metered charge of working fluid is injected through the fill port.
Stage 2: Primary & Secondary Degassing with Fixed-Length Cutting
The pipe is evacuated to remove bulk air (primary degassing), then heated under vacuum so dissolved gas comes out of the fluid (secondary degassing). The pipe is then cut to its final length while still under vacuum, so it is never exposed to atmosphere between degassing and sealing.
Stage 3: Head Welding & Final Testing
The cut end is sealed by TIG welding under vacuum, and the finished pipe passes through an in-line test station that checks thermal performance before it is released for packing.
Applications
This line configuration suits manufacturers producing heat pipes for consumer electronics thermal modules, laptop and server heat sinks, LED lighting, and general electronics cooling, where volume and consistent per-pipe quality matter more than one-off custom geometry.
Why Choose Cooling-Thermal
We build each line around your pipe geometry and target output — station count, cycle time, and fixture design are matched to your product before build, and the line is validated on your own pipes before shipment. The line integrates with our standalone powder filling and sintering equipment upstream, and with our testing and inspection stations downstream, so you can scale from a single station to a full line as your volume grows.
The Three Stages of the Automatic Line

Tail Welding and Water Filling

Primary and Secondary Degassing with Fixed-Length Cutting

Reviews
There are no reviews yet.