Product Description
| Parameter Item | Specification/Value |
|---|---|
| Pipe Diameter | Ø4 ~ Ø10 mm |
| Pipe Length | 120 ~ 600 mm |
| Pipe Thickness | 0.2 ~ 0.6 mm |
| Vacuum Degree | 6×10⁻¹τ |
| Water Volume Tolerance | ±0.2% |
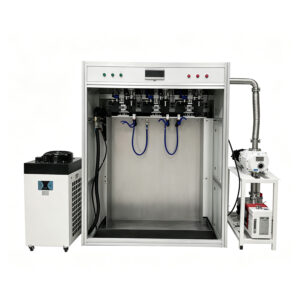
| Coarse Extraction Configuration | Oil Pump – 250 m³ |
| Fine Extraction Configuration | Roots Pump – 250 m³ + Diaphragm Pump – 80 m³ |
| Limit Vacuum Value | 0.7×10⁻²τ |
| Degassing Vacuum Value | 0.3 ~ 0.4 τ |
| Extracted Water Volume Tolerance | ±0.02 g |
| Extraction Speed per Unit | 670 L/min |
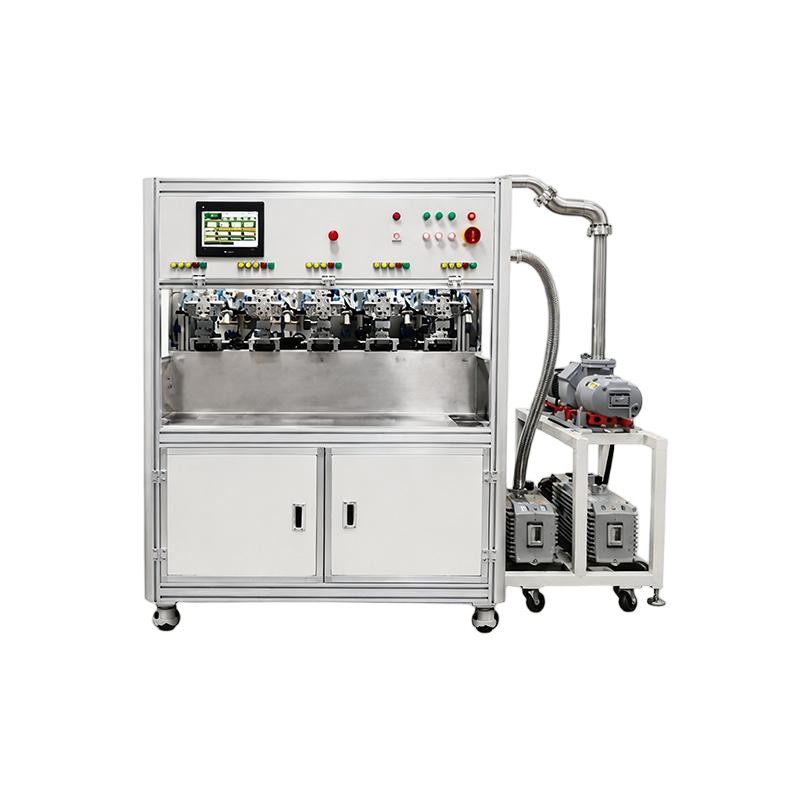
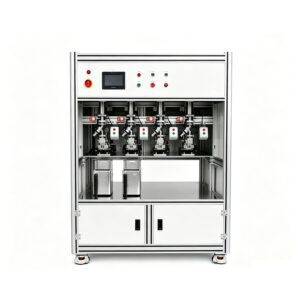
The machine supports pipe diameters from Ø5 to Ø8mm and pipe lengths from 130 to 500mm, with a heating temperature up to 250°C and a heating length of up to 60mm. The U-shaped riveting uses 70kg oil pressure through a Ø50×30mm riveting cylinder. It achieves a yield rate of 99.8%. The machine operates on 380V power with a compact footprint of 1,000 × 1,120 × 1,400mm, and is equipped with 2 workstations.
This machine is also used as an R&D sample-making machine for heat pipe prototyping and small-batch process validation before full production line commissioning.
Advantages of the Heat Pipe Degassing & Sealing Machine
Integrated Degassing and Welding in One Cycle
The machine combines heating degassing, U-shaped riveting, and cutting in a single automated sequence. The heat pipe does not need to be transferred between a separate degassing machine and a separate welding machine. This eliminates the air re-entry risk that occurs during inter-machine transfer, and reduces handling-related damage to thin-wall copper tubes.
99.8% Yield Rate
The machine achieves a 99.8% yield rate through its integrated process design — top-loading with automatic push to riveting position, immediate cutting after riveting, and temperature-and-time controlled heating degassing. The elimination of manual transfer between stations removes the two most common yield loss sources: air re-entry and handling deformation.
Adjustable Degassing End Position
The position of the degassing end can be adjusted by positioning control, accommodating different heat pipe lengths and degassing end configurations within the Ø5–Ø8mm diameter range. This flexibility allows the same machine to handle multiple heat pipe product variants without fixture changeover.
R&D and Sample Making Capability
The machine serves as an R&D sample-making machine for heat pipe prototyping. Its 2-station configuration and compact footprint (1,000 × 1,120 × 1,400mm) make it suitable for small-batch process validation, new product development, and parameter tuning before committing to full production line equipment.
How the Heat Pipe Degassing Welding Machine Works
Step 1 — Top Loading and Automatic Positioning
The heat pipe is placed into the machine from the top. The machine automatically pushes the tube to the riveting position. The degassing end position is set through the positioning control to match the specific pipe length and degassing end geometry.
Step 2 — Heating Degassing
The heating system raises the degassing end temperature to the set point (up to 250°C) over the set heating length (up to 60mm). Heating is controlled by both temperature and time parameters. The heat drives non-condensable gas and moisture out of the heat pipe interior through thermal expansion of the working fluid. The heating temperature and duration are set based on the pipe diameter, wall thickness, and working fluid type.
Step 3 — U-Shaped Riveting and Sealing
Immediately after degassing, the riveting mechanism applies 70kg oil pressure through the Ø50×30mm riveting cylinder to crimp the degassing end into a U-shaped seal. The riveting occurs while the tube is still in the degassed state — there is no transfer step between degassing and sealing, so no atmospheric air can re-enter the tube before the seal is completed.
Step 4 — Cutting and Discharge
Immediately after riveting, the cutting mechanism trims the crimped waste end to the final pipe length. The completed heat pipe — degassed, sealed, and cut to length — is discharged and ready for the next production step (hot pressing, bending, or performance testing).
Where the Degassing Sealing Machine Fits in Your Heat Pipe Production Line
The heat pipe heating degassing welding machine is positioned at the degassing and sealing stage of the heat pipe production sequence — after water injection and before hot pressing and bending.
In a typical production flow:
Tube Cutting → Shrinking → Powder Filling → Sintering → Water Injection → Degassing & Sealing (this machine) → Hot Pressing → Bending → Straightening → Leak Testing → Performance Testing
This machine replaces two separate stations (a standalone heating degasser + a standalone welder) with a single integrated unit. It is particularly suited for production lines where floor space is limited, where the product mix includes multiple heat pipe variants in the Ø5–Ø8mm range, or where the line is being set up for R&D and small-batch validation before scaling to full production volume.
The machine can be ordered as a standalone unit or alongside CoolingThermal’s other heat pipe production equipment — including pipe cutting machines, tube shrinking machines, powder filling machines, sintering furnaces, water injection machines, hot press machines, bending machines, and testing equipment.
How the Degassing & Sealing Process Works

Vacuum degassing

Fix length

Reviews
There are no reviews yet.